Precision Inconel 718 CNC Machining Services
PRECI5 provides specialized CNC machining services for Inconel 718, a nickel-chromium superalloy essential for high-performance applications in aerospace, power generation, and chemical processing. We combine advanced 5-axis Inconel machining, rigid process control, and comprehensive inspection to meet the stringent requirements of components subjected to extreme temperatures and corrosive environments.
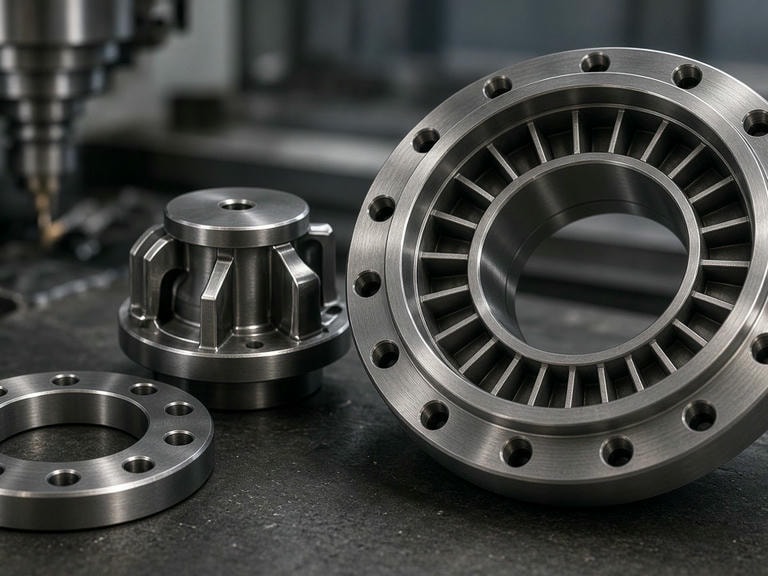
Process Verification
5-Axis Inconel Machining | Tight Tolerances up to ±0.003 mm
The Technical Challenges of Inconel 718 Machining
Inconel 718 is classified as a difficult-to-machine superalloy due to extreme shear resistance, rapid work hardening, and low thermal conductivity. Overcoming these characteristics requires targeted cutting strategies, balanced thermal management, and rigid machine tools.
Work Hardening Control
Inconel 718 hardens rapidly under tool pressure. If cutting edges rub rather than shear or if feed drops, surface hardness exceeds cutter capability, resulting in rapid tool chipping and surface degradation.
Low Thermal Conductivity
Unlike carbon steels or light alloys, Inconel 718 traps cutting heat directly at the shearing zone. Localized temperatures frequently exceed 800°C, accelerating crater wear and localized plastic deformation.
High Shear Strength & Wear
The high yield strength of nickel-chromium alloy imposes excessive mechanical loads onto cutting edges, inducing notch wear, burr formation, and risk of deflection on thin-walled profiles.
5-Axis Inconel Machining Fleet
PRECI5 operates 114 production and supporting units certified to ISO 9001, IATF 16949, and ISO 14001. Our plant in Shenzhen is purpose-built to handle complex high-temp alloys with consistent repeatability.
Facility Scale
Core Machining & Inspection Equipment Matrix
| Equipment Type | Qty | Working Envelope (X, Y, Z) | Spindle / Rating | Positioning Accuracy |
|---|---|---|---|---|
| Mazak C600 5-Axis Centers | 8 | 900 × 900 × 700 mm | 24,000 rpm | ±0.003 mm |
| ZEISS CMM Measuring Unit | Multi | 700 × 700 × 600 mm | Scanning / Optical | Sub-micron verification |
| Precision Cylindrical & Surface Grinding | Dedicated | Shaft & Bearing Profiles | High Rigidity | Ra 0.2 μm / ±0.002 mm |
| Hardness Inspection & Material Verification | In-house | Rockwell & Vickers + XRF | Direct Readout | Precipitation / Solution Verification |
Multi-axis integration enables single-setup multi-face profiling, preventing datum migration and minimizing geometric tolerance stack-up across demanding critical faces.
Inconel 718 Material Conditions & Technical Baselines
Inconel 718 (UNS N07718) is an age-hardenable nickel-chromium-iron-molybdenum superalloy combining high corrosion resistance with extraordinary yield, tensile, and creep-rupture strength up to 700°C (1300°F). Cutting parameters differ significantly between solution-annealed and precipitation-aged states.
Solution-Treated Condition
Lower bulk hardness, higher ductility. Susceptible to galling, rapid edge build-up, and continuous chip wrapping if feeds and chip breakers are sub-optimal.
Precipitation-Hardened (Aged) Condition
Increased hardness (36–44 HRC) and extreme shear strength. Requires lower surface speeds, high-performance ceramic or whisker-reinforced tooling, and rigid clamping setups.
| Density | 8.19 g/cm³ |
| Tensile Strength (Ultimate) | ~1240 MPa |
| Yield Strength (0.2% Offset) | ~1030 MPa |
| Hardness (Aged Condition) | 36–44 HRC |
| Elongation at Break | 12–25% |
| Temperature Capability | Up to 700°C (1300°F) |
Quality Control, Inspection & Secondary Processes
Guaranteeing microstructural stability, geometrical accuracy, and surface conformity across all flight-critical and pressure-retaining components.
ZEISS CMM Metrology
Direct CAD-to-part verification across complex 3D profiles utilizing a 700 × 700 × 600 mm tactile and optical scanning setup.
Hardness & Microstructure
Benchtop Rockwell and Vickers testers verify post-machining condition and precipitation aging conformity across all raw stock lots.
Precision Grinding & Honing
External/internal cylindrical grinding and extrusion honing yield Ra 0.2 μm or finer finishes for seal registers and rotating turbine shafts.
Micro-Hole Machining
Specialized deep-hole and micro-hole drilling tailored for cooling orifices, pressure channels, and fluid manifolds in combustion systems.
1. Tool Path Optimization
Eliminating dwells and non-cutting engagements prevents localized surface work hardening and preserves dimensional stability.
2. High-Rigidity Fixturing
Custom dedicated hydraulic and mechanical clamping absorbs extreme radial cutting forces and dampens vibration.
3. DFM & Material Analysis
Our engineering department evaluates wall thickness, fillet transitions, and internal radii to ensure production feasibility.
Inconel CNC Machining: Technical FAQ
Answers to frequent engineering and procurement questions regarding our Inconel 718 machining capabilities.
Send Your Inconel 718 Drawing & Material Condition
Upload your parts drawings and technical specifications. Our engineering team conducts a thorough DFM check, confirms material state requirements (annealed vs aged), and provides a transparent quote with production lead time.