Precision Aluminum 5083 CNC Machining
PRECI5 provides high-precision 5083 aluminum machining and large structural component milling for marine vessels, industrial equipment, and corrosive operational environments. Leveraging our fleet of 114 production machines—including 8 Mazak C600 5-axis centers—we manufacture high-integrity 5083 precision parts with superior dimensional stability.
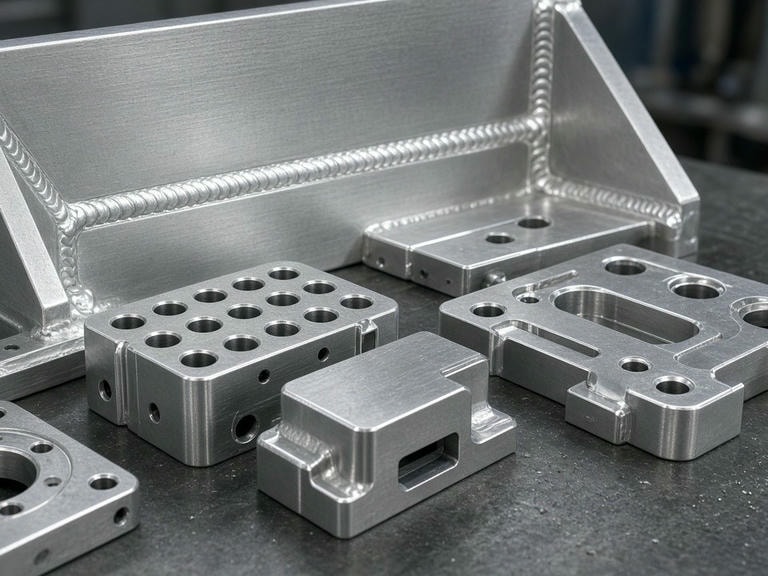
Why Specify Aluminum 5083 for Machined Components?
Aluminum 5083 is a non-heat-treatable alloy celebrated for exceptional resistance to saltwater corrosion and extreme cryogenic resilience. It retains mechanical strength post-welding and resists stress cracking, making it the premier choice for marine hull fittings, offshore pressure housings, and heavy industrial structures.
Mechanical Properties by Temper Classification
Values vary according to temper and cross-section thickness. Select a temper tab to preview standard parameters:
| Temper | Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | Hardness (Brinell) | Elongation (%) |
|---|---|---|---|---|---|
| 5083-O (Annealed) | 2.66 | 270 – 350 | 125 – 200 | ~75 HB | 16 – 22% |
| 5083-H111 | 2.66 | 275 – 350 | 125 – 210 | ~78 HB | 15 – 20% |
| 5083-H112 | 2.66 | 280 – 360 | 130 – 240 | ~80 HB | 12 – 18% |
| 5083-H321 (Marine Spec) | 2.66 | 310 – 385 | 215 – 295 | 85 – 95 HB | 10 – 16% |
*Important Note: Mechanical figures are indicative of generic plate and extrusion stock. Please define your target temper (e.g., O, H111, H112, H321) on technical drawings during quotation.
Large-Scale 5083 CNC Machining Equipment
Handling 5083 aluminum plates and forgings requires robust machine rigidity, active chip evacuation, and thermal control to offset work hardening and residual stress. Our 114-machine facility integrates multi-axis Mazak technology to handle parts ranging from palm-sized marine connectors to massive structural flanges.
| Equipment Model | Kinematic Configuration | Total Fleet | Machine Travel Limits (X × Y × Z) | Positioning Precision |
|---|---|---|---|---|
| Mazak C600 | Simultaneous 5-Axis | 8 Units | 900 × 900 × 700 mm | ±0.003 mm |
| Mazak VCN-430AL | High-Speed 4-Axis | 39 Units | 560 × 430 × 510 mm | ±0.003 mm |
| Mazak HCN5000 | Horizontal Machining Center | 2 Units | 560 × 430 × 510 mm | ±0.003 mm |
| Mazak QTC100MY | Turn-Mill Center with Y-Axis | 10 Units | X: 300 mm / Z: 500 mm | ±0.003 mm |
Setup Minimization for Complex 5083 Geometries
By deploying 5083 CNC machining on our 5-axis Mazak C600 units, we process multi-angled surfaces, deep pockets, and undercut features in fewer clampings. Reducing part reclamping prevents cumulative datum drift, eliminates operator repositioning inaccuracies, and assures precise concentricity across large structural bulkheads.
- ✓ Minimizes distortion caused by internal residual stresses during roughing.
- ✓ Maintains tight true-position tolerances across compound face angles.
- ✓ Enables high-efficiency trochoidal toolpaths for deep cavities.
Quality Control & Metrology Verification
Marine and high-pressure industrial applications cannot tolerate material impurities or dimensional deviations. Our climate-controlled inspection center uses optical and contact measurement equipment to validate critical tolerances before packing and international dispatch.
Engineering Support & DFM Consultation
From initial EVT and DVT pilot runs to recurring volume manufacturing, our Shenzhen engineering staff analyzes your 3D CAD files for tool reach, wall-thickness integrity, and raw billet optimization. We proactively identify potential machining vibration points and advise on temper selection to deliver cost-efficient, production-ready 5083 precision parts.
Request a Fast Machining Quote
Our engineering team is prepared to evaluate your project. To ensure rapid DFM analysis and an accurate quote, please provide full documentation:
Submit Your Engineering RFQ
Attach drawings and specify batch quantities, required temper, and tolerance callouts.