Precision UHMW-PE CNC Machining Services
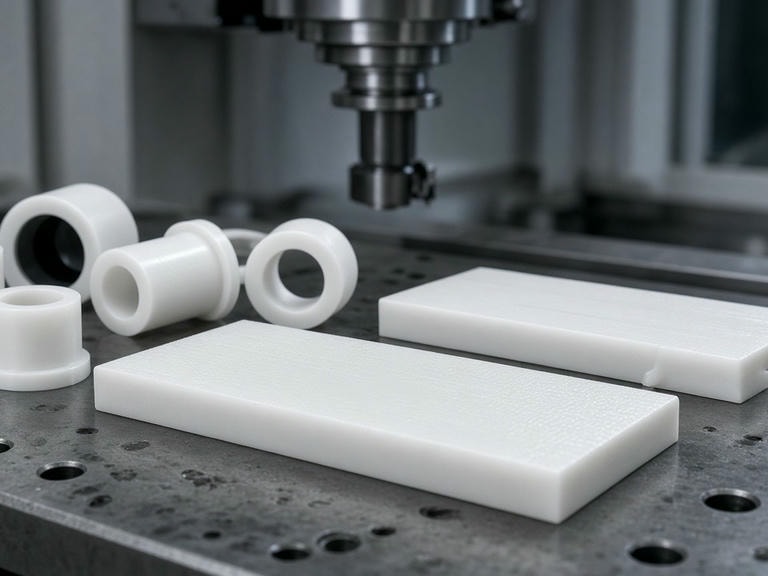
PRECI5 delivers industrial-grade UHMW CNC machining solutions engineered for wear guides, custom sliders, conveyor systems, and automation components. Combining 5-axis machining capability with plastic-specific thermal control, we maintain dimensional stability across complex geometries.
Material Specification
Material Characteristics: Why UHMW-PE?
Ultra-High Molecular Weight Polyethylene provides an optimal combination of low coefficient of friction, high impact resistance, and continuous lubricity. It outperforms standard engineering thermoplastics in abrasive material handling and sanitary environments.
| Property | Typical Reference Value | Engineering Significance |
|---|---|---|
| Density | 0.93 - 0.94 g/cm³ | Lightweight, floats on water, lowers assembly inertial loads |
| Tensile Strength | 20 - 30 MPa | Yield resilience with high energy absorption capacity |
| Continuous Service Temp | 80°C - 90°C | Optimal for ambient and low-temperature production lines |
| Water Absorption | < 0.01% | Hydrophobic, eliminates swelling in wet washdown zones |
| Coefficient of Friction | 0.10 - 0.22 | Self-lubricating profile prevents equipment galling |
| CTE (Expansion) | 1.5 - 2.0 × 10⁻⁴/K | High expansion coefficient requires engineered clearance |
*Values represent standard virgin UHMW-PE typical reference data. Modified grades (ceramic-filled, anti-static, or MoS2-filled) will differ.
Target Component Applications
Technical Control
Engineering Challenges in UHMW-PE Machining
UHMW-PE exhibits distinct physical behaviors compared to metals and rigid engineering plastics. Successful UHMW CNC machining requires proactive countermeasures for elastic recovery, heat sensitivity, and mechanical compliance.
Material Softness & Compliance
UHMW-PE yields under standard jaw pressure. Conventional metalworking chucks cause localized deformation, which results in out-of-round bores or arched flats once the part is released.
High CTE & Heat Dissipation
With a CTE up to ten times greater than mild steel and low thermal conductivity, heat builds up rapidly at the cutting interface. This can induce surface melting, gumming, and thermal expansion during cutting.
Internal Stress & Post-Cut Warping
Extruded and compression-molded stock contains differential residual stresses. Asymmetrically clearing material on long rails or thin-walled profiles causes immediate warping.
Production Infrastructure
Machining Capacity & Equipment
PRECI5 operates an industrial facility equipped with 114 machine tools. Our dedicated CNC plastic routing, turning, and multi-axis centers process raw billets up to large-scale structural guides with stable repeatability.
Process Rule: UHMW-PE requires sharp cutting edges with zero negative rake to prevent plastic burrs. Dedicated polymer tool libraries ensure no contamination or cross-work hardening from metal processing.
| Capability | Equipment Model | Axis / Capacity |
|---|---|---|
| 5-Axis Machining | Mazak C600 | 900 × 900 × 700 mm |
| 4-Axis Milling | Mazak VCN-430AL | 560 × 430 × 510 mm |
| CNC Turn-Mill | Mazak QTC100MY | Max Dia. Φ350 mm |
| CNC Turning | Mazak QTE100 | Max Dia. Φ350 mm |
Quality & Standards
Dimensional Inspection & Factory Standards
Because UHMW-PE expands and flexes under localized pressure and temperature variance, quality assurance requires disciplined thermal soaking prior to final inspection.
Climate-Controlled Metrology
Parts are conditioned at 20°C (±1°C) before final measurement to ensure ambient heat expansion does not skew tight tolerance verification on ZEISS CMMs and 2.5D optical systems.
Contact-Free & Low-Force Probing
Tactile probing uses tuned stylus contact forces to prevent point-deflection on compliant UHMW surfaces, paired with non-contact video measurement for delicate edge profiles.
Facility Certifications
PRECI5 holds ISO 9001, IATF 16949, and ISO 14001 certifications. Full material traceability, raw stock mill certificates, and lot inspection reports are standard deliverables.
Design For Manufacturing
DFM Recommendations for UHMW-PE Parts
Review our quick engineering guidance for optimizing machining time, surface quality, and part stability when designing components with UHMW-PE.
Start Your Project
Send Your UHMW-PE Drawing & Tolerance Requirements
Upload or submit your CAD models (STEP, IGES, DXF) with 2D drawings showing critical linear and geometric tolerances. Our team provides comprehensive DFM evaluation, cycle time estimates, and pricing within 24 hours.