Precision Aluminum 5052 CNC Machining Services
PRECI5 provides high-precision 5052 aluminum CNC machining, specializing in complex geometries and tight-tolerance components. Operating 114 production units in Shenzhen—including 8 Mazak C600 5-axis and 39 Mazak VCN-430AL 4-axis machining centers—we ensure that your 5052-H32 projects meet demanding engineering requirements from initial prototype to volume production.
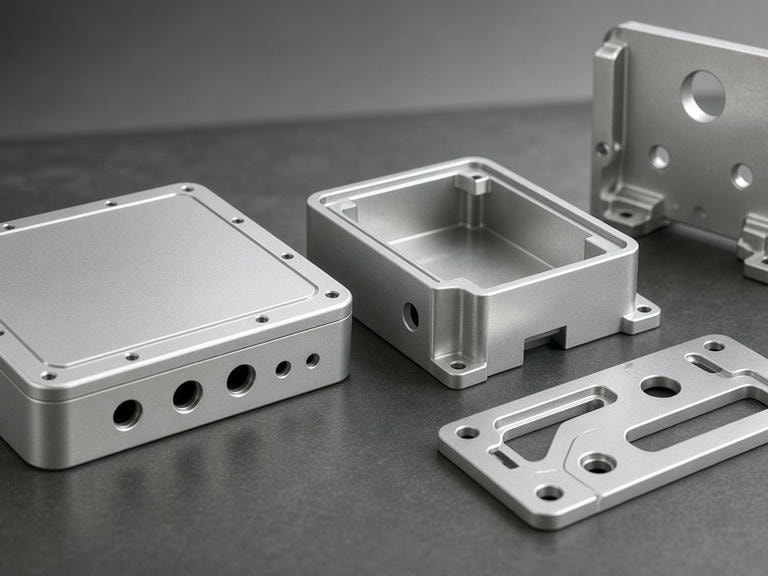
Why Choose Aluminum 5052-H32 for Machining?
Aluminum 5052 is a non-heat-treatable magnesium-alloyed aluminum known for outstanding resistance to atmospheric and saltwater corrosion. The H32 temper strain-hardens the material followed by partial annealing, striking a dependable equilibrium between tensile strength and cold formability.
For specialized 5052-H32 machining, the alloy provides notable weldability and ductile behavior for secondary bending, micro-hole drilling, or deep forming. It serves as an industry standard across electronic chassis, instrument housings, marine enclosures, and sensitive process equipment where raw corrosion resilience outperforms standard architectural alloys.
Key Industrial Applications
Electronic enclosures, marine hardware, control instrument panels, pneumatic manifolds, hydraulic tubing, and chemical processing fixtures.
Typical Material Properties: 5052-H32
ASTM B209 / EN 485| Mechanical / Physical Property | Standard Metric Value |
|---|---|
| Density | 2.68 g/cm³ |
| Tensile Strength (Ultimate) | 230 MPa |
| Yield Strength (0.2% Offset) | 195 MPa |
| Hardness (Brinell) | 60 HB |
| Elongation at Break | 12% |
Values are representative engineering baselines for 5052-H32 plate and bar stock under ambient conditions.
Aluminum 5052 vs. 6061: Selecting the Right Alloy
Selecting between 5052-H32 and 6061-T6 depends primarily on structural load, environmental exposure, and required forming methods.
| Evaluation Criteria | Aluminum 5052-H32 | Aluminum 6061-T6 |
|---|---|---|
| Machinability | Good (can be gummy; requires optimized chip-breakers and high-speed tooling) | Excellent (short chips, fast feed rates, ideal for high-speed hogging) |
| Corrosion Resistance | Superior (outstanding bare exposure in saline and marine settings) | Good (standard practice requires protective anodizing in harsh exposures) |
| Weldability | Excellent (low cracking susceptibility with 5356 filler) | Good (weld heat reduces localized temper strength) |
| Mechanical Strength | Moderate (Yield ~195 MPa; Tensile ~230 MPa) | High (Yield ~276 MPa; Tensile ~310 MPa) |
| Primary Applications | Marine enclosures, electronic chassis, hydraulic piping, formed brackets | Heavy structural parts, aerospace fixtures, automotive frames, precision robotics |
Unsure which alloy aligns best with your deflection limit, post-machining bending, or surface finish targets?
Consult Our Engineering Team →Advanced Manufacturing Infrastructure
Our Shenzhen facility is engineered for complex 5052 aluminum CNC machining. Multi-axis Mazak centers reduce handling, maintain tight geometric tolerances, and stabilize the alloy during aggressive chip evacuation.
Multi-axis positioning repeatability guaranteed across high-speed milling cycles.
8 x Mazak C600
Work envelope up to 900 × 900 × 700 mm; 24,000 RPM high-speed spindles for complex contoured 5052 housings.
39 x Mazak VCN-430AL
High-rigidity vertical machining centers tailored for rapid multi-face indexing and repeat part consistency.
2 x Mazak HCN5000
Dual-pallet continuous production designed for high-volume 5052-H32 enclosures and valve manifolds.
22 x Turn-Mill Units
10 x Mazak QTC100MY and 12 x Mazak QTE100 for single-setup cylindrical components with live tooling.
Metrology & Inspection Protocol
Because 5052-H32 can be susceptible to deflection during machining, dimensional verification and surface integrity checks are integrated directly into our workflow.
Coordinate Metrology
Equipped with a climate-controlled ZEISS CMM (700 × 700 × 600 mm) and Sirius CMM systems alongside 2.5D optical measurement projectors for comprehensive GD&T reporting.
Material & Surface Validation
XRF alloy verification confirms compliant chemical composition before raw stock enters spindle operations. Mitutoyo roughness testers verify Ra values down to 0.4 µm.
Hardness & Coating Checks
Rockwell and Vickers hardness testers verify cold-worked temper integrity. Dedicated thickness gauges validate anodized, alodine, or chemical conversion layers.
DFM Feedback & Prototype-to-Scale Support
Machining 5052-H32 requires tailored tool geometry, feed rate modulation, and rigid clamping setups to counter edge-burr formation and thermal expansion. During the NPI (New Product Introduction) phase, our technical team evaluates CAD files to identify tool radius limits, thin-wall risks, and assembly interference.
- • Comprehensive DFM reports provided within 24 hours of CAD submission.
- • Tooling path optimization for reduced cycle times and burr-free chamfers.
- • Seamless transition from 1-off prototypes to repeat multi-thousand-part production runs.
5052 Machining FAQ
Upload Your 5052 Aluminum Drawing
Send your 2D and 3D files to our engineering team. We deliver complete manufacturability evaluations, tooling plans, and binding quotations within 24 hours.