Precision POM / Delrin CNC Machining Services
PRECI5 provides high-precision acetal CNC machining for complex components requiring tight tolerances, dimensional stability, and low-friction wear surfaces. Powered by 8 Mazak C600 5-axis and 39 Mazak VCN-430AL 4-axis machining centers, we produce production-grade POM-C and Delrin® parts for demanding industrial applications.
Material Engineering
Acetal Resin Selection: POM-C vs. POM-H (Delrin®)
Polyoxymethylene offers balanced rigidity, low friction, and exceptional machinability. Choosing between Copolymer (POM-C) and Homopolymer (POM-H / Delrin®) depends on chemical exposure, mechanical load, and operating temperature profiles.
POM-C (Acetal Copolymer)
e.g., Sustarin® C, Ertacetal®The industry standard for multi-purpose precision machining. Highly resistant to hydrolysis, strong alkalis, and thermal-oxidative degradation, with virtually no center-line porosity.
- Superior resistance to hot water, steam, and alkaline chemicals
- Lower centerline porosity for leak-tight medical and fluid blocks
- Higher dimensional stability in humid operating conditions
POM-H (Acetal Homopolymer)
e.g., DuPont™ Delrin®Characterized by a higher crystalline structure delivering elevated tensile strength, stiffness, and fatigue life for continuous mechanical loads.
- Approx. 10–15% higher tensile strength and flexural modulus
- Exceptional surface hardness and superior long-term creep resistance
- Lower coefficient of friction against metals and other plastics
Quantitative Physical & Mechanical Properties
Standard test conditions (23°C / 50% RH)| Physical Property | Typical Value (POM-C) | Typical Value (Delrin® POM-H) | Machining & Design Significance |
|---|---|---|---|
| Density | 1.41 g/cm³ | 1.42 g/cm³ | Lightweight alternative to brass and aluminum structural elements |
| Tensile Strength | 60–70 MPa | 70–85 MPa | Resists high snap-fit deflection and cyclical mechanical stress |
| Water Absorption (24h) | 0.20% | 0.25% | Minimal swelling ensures tight bore and thread tolerances in liquid service |
| Service Temperature | -40°C to 100°C | -40°C to 90°C | Maintains dimensional and impact stability across thermal excursions |
| Coefficient of Thermal Expansion (CTE) | 110–120 µm/m·K | 100–110 µm/m·K | Strict temperature-controlled cutting environments prevent thermal growth |
Precision Engineering
Target Applications for Delrin & Acetal Machining
Because of its self-lubricating characteristics and high modulus, CNC-machined POM replaces soft metals in critical mechanisms requiring low inertia, zero galling, and electrical isolation.
Precision Sliding Parts
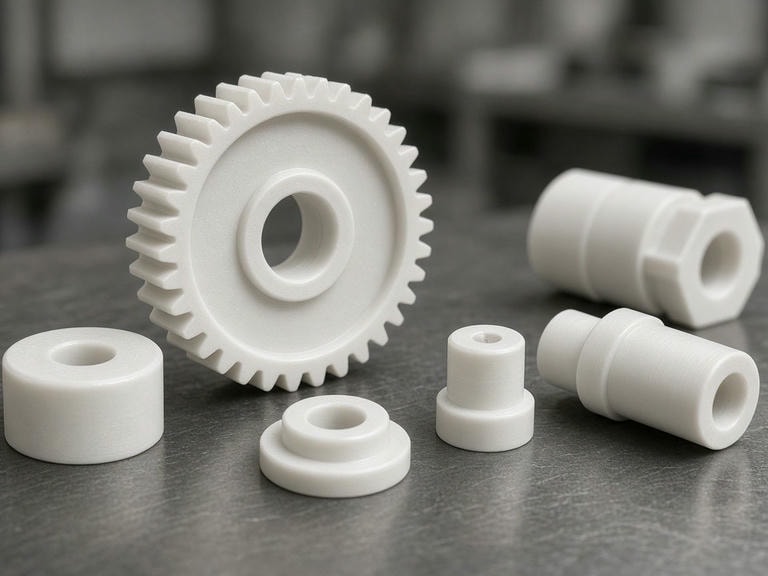
Spur gears, metric drive bushings, lead screw nuts, guide blocks, and cam rollers that operate continuously with dry lubrication and minimal frictional drag.
Automated Fixtures & Jigs
Assembly nests, test sockets, wear strips, and alignment tooling where non-marring, wear-resistant, and non-conductive holding fixtures are mandatory.
Insulating Structures
Switchgear housings, terminal insulators, high-frequency coil bobbins, and electrical standoff brackets providing high dielectric breakdown strength.
Fluid & Medical Manifolds
Microfluidic manifolds, metering valves, flow bodies, and lab automation components requiring accurate reamed holes and chemical rinse resilience.
Mazak 5-Axis Centers & Metrology-Backed Assurance
Machining engineering plastics demands deliberate thermal control, specialized cutting tool geometry, and stress-relieved stock. Our high-speed spindle Mazak machines cut clean chip profiles without inducing localized melting or micro-cracks.
8 Mazak C600 5-Axis Machining Centers
Multi-sided indexing cuts down repositioning setups, securing geometric concentricity, perpendicularity, and true position across complex geometric planes.
39 Mazak VCN-430AL 4-Axis Machines
Rigid 4-axis production cells designed for high-speed continuous milling of POM-C bushings, structural brackets, and deep-pocket tooling.
ZEISS 700 × 700 × 600 CMM Verification
Temperature-stabilized metrology lab verifying 0.003 mm machine positioning precision, GD&T runout, bore roundness, and surface finish compliance.
Technical Machining Standards for Acetal
Our standard operating envelope for tight-tolerance Delrin and POM CNC processing:
Eliminates internal extrusion stresses in thick Delrin plate and rod stock to prevent post-machining warpage and dimensional creep.
Razor-sharp cutting edges with open flute geometry prevent chip re-welding, generating burr-free edges and Ra 0.8 µm surface textures without secondary deburring.
Prevents the workpiece from exceeding thermal thresholds, compensating for POM's 110 µm/m·K coefficient of thermal expansion during precision boring.
Every critical dimension, bore diameter, thread engagement, and keyway is mapped against your CAD file before batch release.
Upload Your POM / Delrin Drawing
Send your 3D CAD files (STEP, IGES, SLDPRT) and 2D drawings (PDF with GD&T) to our engineering team. We deliver complete DFM feedback, cycle time evaluation, and formal quotes within 24 hours.
Request an Acetal Machining Quote
Complete the project scope below. Our technical sales engineers will contact you shortly.