Large-Format 5-Axis CNC Machining Services
PRECI5 delivers precision large format 5 axis CNC machining for complex, multi-surface components. Operating from our advanced facility in Shenzhen, we help engineering and procurement teams bypass 3-axis boundaries to achieve micron-level positional accuracy, streamline setups, and accelerate cycle times for large CNC machining projects in China.
Core Capacity Snapshot
Our Large-Format Machining Capacity
Our dedicated workshop runs 8 high-performance Japanese Mazak C600 5-axis machining centers. These premium machine tools are purpose-engineered for rigidity, dynamic balance, and thermal stability when processing substantial, multi-faceted structural components.
| Specification Parameter | Verified Floor Capability |
|---|---|
| Machine Model | Mazak C600 (8 Units Fleet) |
| X-Axis Travel | 900 mm |
| Y-Axis Travel | 900 mm |
| Z-Axis Travel | 700 mm |
| Rotary Axis (C / B) | 360° Continuous Rotation |
| Spindle Speed | 24,000 rpm High-Speed Direct-Drive |
| Tool Magazine Capacity | 30 Tools Auto-Changer |
| Machine Listed Precision | 0.003 mm |
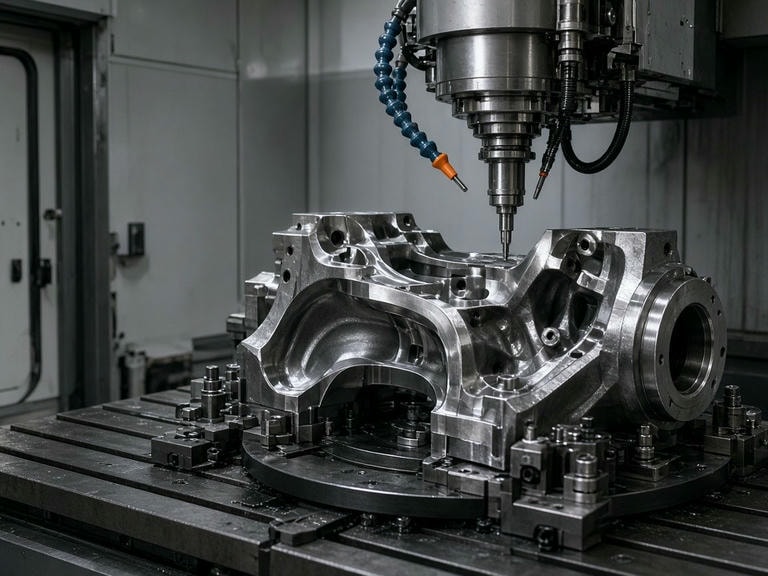
Advanced Large 5 Axis Machining in China
Equipped to mill aerospace structural members, robotic arm knuckles, energy flow manifolds, and large semiconductor chambers with minimal repositioning setups.
Why Single-Setup 5-Axis Matters
- Eliminates Stack-up Errors: Machining multiple compound angles in one clamping maintains true datum references.
- Shorter Rigid Tooling: Rotary head positioning lets cutters reach deep cavities without excessive tool deflection.
- Surface Continuity: Continuous 5-axis contouring produces uniform transitional blending across complex freeform geometries.
Supporting Processes for Large Components
Large-format components demand more than raw milling. We combine secondary machining, precision cylindrical finishes, and coordinate metrology under one roof to eliminate subcontracting delays and transit-related damage.
Turn-Mill & Turning
Equipped with 10 Mazak QTC100MY turning centers to profile concentric shafts, large flange seatings, and radial sealing grooves before or after 5-axis operations.
Horizontal Machining
Twin-pallet Mazak HCN5000 horizontal machining centers provide deep-hole coring and repetitive pocketing for high-volume, prismatic casting blocks.
Grinding & Honing
Critical bearing journals and mating faces achieve micro-inch surface finishes and roundness via precision cylindrical, surface grinding, and internal bore honing.
Metrology & CMM
Full geometric dimensioning and tolerancing (GD&T) verified in an environmentally stable lab on our ZEISS CMM (700 × 700 × 600 mm) and Sirius CMM units.
Engineering Support & Pre-Production DFM
Large parts exhibit elevated raw material costs and heightened risk of stress-relief distortion. Before any cutter engages your raw billet or casting, our engineering team executes rigorous tool-path simulation and DFM review:
Clamping & Rigidity Simulation
Analyzing cutting forces against thin-walled sections or heavy overhangs to prevent chatter, deflection, or tool vibration.
Kinematic Interference Verification
Simulating B/C rotary tilt boundaries to confirm the spindle head avoids collisions with part corners and customized clamping vices.
Cost-Saving Stock Optimization
Advising on radii standards, standardized internal corner reliefs, and staged roughing sequences that cut cycle time and material waste.
Multi-Tier Quality Compliance
Our operational workflows adhere to internationally recognized industrial certifications, giving global clients full trace control over material chemistry, heat treatment, and dimension validation.
Full CMM Inspection Reports, Material Test Certs (3.1 / Mill Test), and First Article Inspection (FAI) reports available upon request.
Large-Part RFQ Feasibility Checklist
To receive a comprehensive kinematic review, cycle-time estimate, and accurate DFM feedback for your large CNC machining requirements, please review our recommended submission parameters:
Specify the full bounding box (L × W × H in mm) of the raw billet or cast blank to confirm axis limits.
Material alloy grade, supply condition (forged, plate billet, or sand casting), and target hardness criteria.
Approximate mass per unit to evaluate table payload limits, lifting requirements, and rigid clamping setups.
Indicate designated datum surfaces (A, B, C) and alignment pins necessary to maintain overall assembly consistency.
Any features tighter than standard ISO 2768-m, positional true position tolerances, or micro-inch finishes.
Clarify prototype quantities (1-5 pcs), bridge batches, or annual production runs for dedicated tooling design.
Request a Feasibility Review & Quotation
Submit your CAD files (STEP, IGES, Parasolid) and PDF 2D prints detailing tolerance callouts. Our senior manufacturing engineers will analyze your 5-axis geometry and provide an actionable feasibility report and quote.
Upload Technical Drawings & Specs
NDAs strictly observed before reviewing proprietary CAD models.